Blue
 info@boxinsteel.com


Product Categories
Contact Us
Wen zhou boxin steel industry Co., Ltd
Add:4102 Yong Qiang Avenue,Longwan District, Wenzhou. China
Tel:+86-577-86927958
Pho:+8618058896089
Fax:+86-577-86927988
E-mail:info@boxinsteel.com
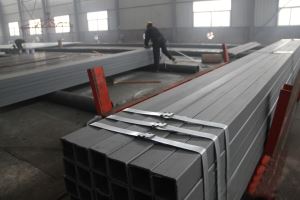
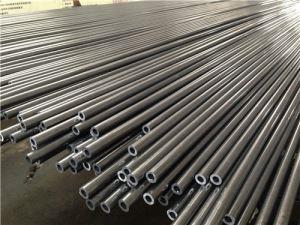
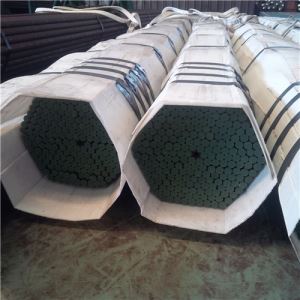
ASTMA A53 Black and Hot Dipped Zinc Coated Welded and Seamless Steel Pipe
Scope:
Covers Seamless and Welded, Black and Hot-Dipped Galvanized nominal (average) wall pipe for coiling, bending, flanging and other special purposes and is suitable for welding. Continuous-Welded pipe is not intended for flanging. Purpose for which pipe is intended should be stated on order.
Materials and Manufacture:
The steel for both seamless and welded pipe shall be made by one or more of the following processes: open-hearth, electric furnace, or basic-oxygen. The weld seam of electric-resistance welded pipe in Grade B shall be heat treated after welding.
Chemical Requirements:
|
Type S |
Type E |
Type F |
||||
|
(electric- |
(furnace- |
|||||
|
Grade A |
Grade B |
Grade A |
Grade B |
Grade A |
||
|
Carbon max. % |
0.25 |
0.30 |
0.25 |
0.30 |
0.3 |
|
|
Manganese % |
0.95 |
1.2 |
0.95 |
1.2 |
1.2 |
|
|
Phosphorous, max. % |
0.05 |
0.05 |
0.05 |
0.05 |
0.05 |
|
|
Sulfur, max. % |
0.045 |
0.045 |
0.045 |
0.045 |
0.045 |
|
|
Copper, max.% |
0.40 |
0.40 |
0.40 |
0.40 |
0.4 |
|
|
Nickel, max. % |
0.40 |
0.40 |
0.40 |
0.40 |
0.4 |
|
|
Chromium, max. % |
0.40 |
0.40 |
0.40 |
0.40 |
0.4 |
|
|
Molybdenum, max. % |
0.15 |
0.15 |
0.15 |
0.15 |
0.15 |
|
|
Vanadium, max. % |
0.08 |
0.08 |
0.08 |
0.08 |
0.08 |
|
Hot-Dipped Galvanizing:
Sets standards for coating of pipe with zinc inside and outside by the hot-dipped process. Weight of coating must not average less than 1.8 oz. per square foot and not less than 1.6 oz. per square foot.
Permissible Variations in Wall Thickness:
The minimum wall thickness at any point shall not be more than 12.5% under the nominal wall thickness specified.
Permissible Variations in Weights per Foot:
Plus or minus 10%
Tensile Requirements:
|
|
Seamless and Electric-resistance-welded |
Continuous-Welded |
|
|
|
Grade A |
Grade B |
|
|
Tensile Strength, min., psi |
48,000 |
60,000 |
45,000 |
|
Yield Strength, min., psi |
30,000 |
35,000 |
25,000 |
Hydrostatic Testing:
Hydrostatic inspection test pressures for plain end and threaded and coupled pipe are specified. Hydrostatic pressure shall be maintained for not less than 5 seconds for all sizes of seamless and electric-resistance-weld pipe.
Mechanical Tests Specified:
Tensile Test -- Transverse required on ERW for NPS 8 and large. Sending Test (Cold) -- STD and XS-NPS 2 and under XXS-NPS 1 1/4 and under.
|
|
Degree of Bend |
Diameter of Mandrel |
|
For Normal A53 Uses |
90 |
12 x nom dia. of pipe |
|
For Close Coiling |
180 |
8 x nom dia. of pipe |
Flattening Test -- NPS 2 and larger STD and XS. (Not required for XXS pipe.)
Lengths:
| Standard Weight | |
|
Single Random -- 16' - 22'. 5% may be jointers. If Plain Ends -- 5% may be 12' - 16'. |
|
|
Double Random -- Shortest Length 22', minimum average for order 35'. |
|
|
Extra Strong and Double Extra Strong |
|
|
Single Random -- 12' -22'. 5% may be 6' - 12'. |
|
|
Double Random (XS and lighter) -- Shortest Length 22', minimum average for order 35'. |
|
|
Lengths longer than single random with wall thicknesses heavier than XS subject to negotiation. |
General Information:
| Couplings -- Applied handling tight. Couplings, 2" and smaller straight tapped, other sizes taper tapped. | |
|
Thread Protection -- Applied to pipe 4" and larger. |
|
|
End Finish (unless otherwise specified) -- |
|
|
STD or XS, or wall thicknesses less than 0.500 in. (excluding XXS): Plain and beveled |
|
|
All XXS and wall thicknesses over 0.500 in.: Plain end square cut. |
a53 Standard Specification for Pipe, Steel, Black and Hot-Dipped, Zinc-Coated, Welded and Seamless1
Diameter & Tolerance:
For pipe ≤ NPS 11⁄2 [DN 40], the outside diameter at any point shall not vary more than 1⁄64 in. [0.4 mm].
For pipe ≥NPS 2 [DN 50], the outside diameter shall not vary more than ±1%.
Galvanized
1), Zinc: The zinc used for the coating shall be any grade of zinc conforming to Specification B 6
2), Weight of Coating—The weight of zinc coating shall be not less than 1.8 oz/ft2[0.55 kg/m2] as determined from the average results of the two specimens taken for test in the manner prescribed in 19.5 and not less than 1.6 oz/ft2[0.49kg/m2] for either of these specimens. And testing the weight of zinc according to ASTMB90
Common Uses:
- Low pressure systems
- Structural applications
- Mechanical components
- Bollards
- Casing